01
SS 304 EIL Approved Pipe
Grade 304, UNS S30400, caps carbon at 0.08% on the 18Cr-8Ni base. Process water, utility headers and general corrosive duty take it.

Developing personalize our customer journeys to increase satisfaction & loyalty of our expansion recognized by industry leaders.
MLTI Private Limited (formerly Moonlight Tube Industries) is a stainless steel EIL approved pipes manufacturer, supplier and exporter, with a combined annual capacity of around 8,000 MT at our plant in Gujarat, India.

EIL is Engineers India Limited, the engineering consultancy whose approved vendor lists govern material procurement on Indian refinery and petrochemical projects. EIL enlistment sits alongside our BIS, IBR and PED approvals. Our Engineers India Limited approved stainless steel pipes are manufactured to ASTM A312 / ASME SA-312 by the seamless and welded (ERW) routes, dimensioned to ASME B36.19M. Seamless pipe carries no joint at all, being produced by piercing a solid billet and drawing it to size, while the welded route rolls strip into a single longitudinal seam. Each pipe is then subjected to either a hydrostatic test or a nondestructive electric test, as SA-312 permits. We hold eleven austenitic grades, 304, 304L, 310, 316, 316L, 316Ti, 321, 321H, 347, 347H and 904L.
Chromium between 16.0 and 26.0% builds the passive film, nickel between 8.0 and 28.0% stabilises the austenite, and molybdenum, titanium or niobium follows the grade. SA-312 specifies minimum tensile and yield strengths of 515 MPa and 205 MPa on the standard grades, 485 MPa and 170 MPa on the L grades, and 490 MPa and 215 MPa on 904L. Seamless 321 over 9.5 mm wall falls to 485 MPa and 170 MPa; seamless 321H over the same wall falls to 480 MPa and 170 MPa.
Bores span 1/8 inch to 10 inches NB across SCH 5S to 80S, in lengths up to 12 metres. Refineries, petrochemicals, gas processing and power plants specify this material. We hold ISO 14001 and ISO 45001 certifications. Every heat ships with an EN 10204 3.1 certificate backed by in-house PMI, tensile and hardness testing; ready stock covers standard sizes.
The specifications of stainless steel EIL approved pipes, from grade coverage to size envelope, are given in the table below.
| Parameter | Value |
|---|---|
| Grades | 304, 304L, 310, 316, 316L, 316Ti, 321, 321H, 347, 347H, 904L |
| Applicable standards | ASTM A312 / ASME SA-312 (Seamless, Welded, and Heavily Cold Worked Austenitic Stainless Steel Pipes); ASME B36.19M for SCH 5S, 10S, 40S and 80S. SCH 20S is supplied to the commercial wall, as B36.19M does not publish it. |
| Nominal bore | 1/8 inch NB (6 mm) to 10 inch NB (250 mm) |
| Schedule | SCH 5S, SCH 10S, SCH 20S, SCH 40S, SCH 80S |
| Wall thickness | 1.24 mm to 12.70 mm, by bore and schedule |
| Manufacturing processes | Seamless and welded (ERW) |
| Section profile | Round (A312 / B36.19M). Square and rectangular hollow sections are supplied to ASTM A554 and are not covered by this specification table. |
| Length | Up to 12 metres; single random, double random and cut lengths |
| Heat treatment | Solution annealed |
| Finish | Mill finish, pickled and passivated |
| End type | Plain end; bevelled on request |
Three questions decide the order on an EIL-consulted project: what the approval covers, which documents evidence it, and how it differs from IBR certification.
Engineers India Limited maintains rigorous vendor lists for projects under its management, restricting procurement exclusively to listed producers. Buying from an EIL Approved Make guarantees that stainless steel pipes meet strict ASTM A312 / ASME SA-312 material standards while passing the consultancy's complete facility evaluation. We deliver these fully certified SS pipes directly against your project line lists and provide the corresponding approval documentation during order placement.
Every consignment of EIL vendor-approved SS pipes leaves with an EN 10204 3.1 mill test certificate recording heat chemistry and mechanical results. Mechanical figures are generated by our in-house tensile and hardness testing, with PMI used for material identification; heat chemistry and any further testing a project specification demands are covered by NABL-approved external laboratories.
EIL approval is commercial enlistment: a consultancy admits a vendor to the procurement pool for refinery and petrochemical work. IBR approval is statutory, arising from the Indian Boiler Regulations, 1950, framed under the Boilers Act, 1923 and continued in force under the legislation that has since replaced it. It applies wherever a pipe enters a boiler or steam service.
As an EIL Approved Manufacturer, we hold EIL and IBR compliance certifications to satisfy both commercial and statutory requirements under a single work order.
Eleven austenitic grades fall within our EIL approved SS pipe range, separated by carbon ceiling, molybdenum addition and stabilising element.
Grade 304, UNS S30400, caps carbon at 0.08% on the 18Cr-8Ni base. Process water, utility headers and general corrosive duty take it.
The L variant caps carbon at 0.035%, protecting weld zones from carbide precipitation where no post-weld anneal is planned.
SS 310 pipe, UNS S31000, holds 24.0 to 26.0% chromium with 19.0 to 22.0% nickel; its oxide scale stays intact in furnace duty.
Grade 316 adds 2.00 to 3.00% molybdenum over 304. Resistance to chloride pitting is the result that cooling water circuits require.
UNS S31603 pairs that molybdenum with a 0.035% carbon ceiling at a 485 MPa tensile minimum. Welded refinery utility circuits specify it.
Titanium stabilisation, at five times the combined carbon and nitrogen content, lets 316Ti resist sensitisation through service held above 500°C.
Grade 321, UNS S32100, resists intergranular attack between 425 and 815°C, the refinery heater window, through the same titanium chemistry.
A raised carbon band of 0.04 to 0.10% gives 321H the creep strength required in superheater and high-temperature steam piping.
Niobium replaces titanium in grade 347, UNS S34700, and the carbide it forms survives repeated thermal cycling in chemical plant piping.
The H version of 347 carries a higher carbon band for stress rupture strength in power station steam circuits.
Grade 904L, UNS N08904, combines 4.0 to 5.0% molybdenum with 1.00 to 2.00% copper for dilute sulphuric acid service. Atmospheric duty doesn't need it; 304 serves at a lower cost.
SA-312 recognises two manufacturing processes: seamless and welded. Our welded output is produced by electric resistance welding, which SA-312 permits because no filler metal is added. Round is the only profile with SA-312 dimensions; square and rectangular hollow sections fall under a separate specification and are covered below.

Seamless pipe begins as a pierced billet drawn over a mandrel, leaving no weld line to inspect or derate. Project classes rated for high pressure or hydrogen duty specify it.

In Electric Resistance Welding (ERW), a continuous steel strip passes through shaping rollers and is joined under high-frequency electric current without filler metal, creating a clean longitudinal seam for SA-312 compliance.
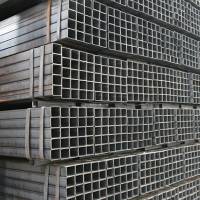 Square
 sections fall outside A312. Mills roll them to ASTM A554, capped at 16 in (406.4 mm) outside dimension. A554 covers mechanical, structural and ornamental tubing, not pressure service, so these sections are supplied for framing and support duty rather than against an EIL piping class. Corners work-harden more than flats. Order by dimension and wall, not NPS.
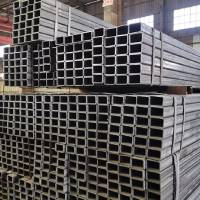 Rectangular
Unequal faces stiffen one axis, which suits pipe-rack cross members and skid frames. These are ASTM A554 structural items, not pressure-carrying pipe. A554 allows ±10% on the wall. Put corner radius, twist and flatness on the drawing.

Round is the only profile with SA-312 dimensions. ASME B36.19M publishes NPS 1/8 through 30; our range runs NPS 1/8 through 10 in schedules 5S through 80S. Pressure loads walls in hoop tension. Heavily cold-worked pipe sits here too.
Our SS pipes span 1/8 inch to 10 inches NB. Outside diameter and schedule wall thickness are given in the table below.
| NB (mm) | NB (inch) | OD (mm) | SCH 5S (mm) | SCH 10S (mm) | SCH 20S (mm) | SCH 40S (mm) | SCH 80S (mm) |
|---|---|---|---|---|---|---|---|
| 6 | 1/8 | 10.3 | - | 1.24 | 1.50 | 1.73 | 2.41 |
| 8 | 1/4 | 13.7 | - | 1.65 | 2.00 | 2.24 | 3.02 |
| 10 | 3/8 | 17.1 | - | 1.65 | 2.00 | 2.31 | 3.20 |
| 15 | 1/2 | 21.34 | 1.65 | 2.11 | 2.30 | 2.77 | 3.75 |
| 20 | 3/4 | 26.7 | 1.65 | 2.11 | 2.55 | 2.87 | 3.91 |
| 25 | 1 | 33.4 | 1.65 | 2.77 | 3.00 | 3.38 | 4.55 |
| 32 | 1 1/4 | 42.2 | 1.65 | 2.77 | 3.00 | 3.56 | 4.85 |
| 40 | 1 1/2 | 48.3 | 1.65 | 2.77 | 3.00 | 3.68 | 5.08 |
| 50 | 2 | 60.3 | 1.65 | 2.77 | 3.00 | 3.91 | 5.54 |
| 65 | 2 1/2 | 73.0 | 2.11 | 3.05 | 4.00 | 5.16 | 7.01 |
| 80 | 3 | 88.9 | 2.11 | 3.05 | 4.00 | 5.49 | 7.62 |
| 100 | 4 | 114.3 | 2.11 | 3.05 | 4.50 | 6.02 | 8.56 |
| 125 | 5 | 141.3 | 2.77 | 3.40 | 5.00 | 6.55 | 9.53 |
| 150 | 6 | 168.3 | 2.77 | 3.40 | 6.35 | 7.11 | 10.97 |
| 200 | 8 | 219.1 | 2.77 | 3.76 | 6.35 | 8.18 | 12.70 |
| 250 | 10 | 273.1 | 3.40 | 4.19 | 6.35 | 9.27 | 12.70 |
Project tonnage and freight are both computed from mass per metre. The kilogram-per-metre weight for each bore and schedule appears in the table below.
| NB (mm) | NB (inch) | OD (mm) | SCH 5S (kg/m) | SCH 10S (kg/m) | SCH 20S (kg/m) | SCH 40S (kg/m) | SCH 80S (kg/m) |
|---|---|---|---|---|---|---|---|
| 6 | 1/8 | 10.3 | - | 0.28 | 0.33 | 0.37 | 0.47 |
| 8 | 1/4 | 13.7 | - | 0.49 | 0.58 | 0.63 | 0.80 |
| 10 | 3/8 | 17.1 | - | 0.63 | 0.74 | 0.85 | 1.10 |
| 15 | 1/2 | 21.34 | 0.80 | 1.00 | 1.08 | 1.27 | 1.62 |
| 20 | 3/4 | 26.7 | 1.03 | 1.28 | 1.52 | 1.68 | 2.20 |
| 25 | 1 | 33.4 | 1.30 | 2.09 | 1.94 | 2.50 | 3.24 |
| 32 | 1 1/4 | 42.2 | 1.65 | 2.70 | 2.90 | 3.38 | 4.47 |
| 40 | 1 1/2 | 48.3 | 1.91 | 3.11 | 3.35 | 4.05 | 5.41 |
| 50 | 2 | 60.3 | 2.40 | 3.93 | 4.24 | 5.44 | 7.48 |
| 65 | 2 1/2 | 73.0 | 3.69 | 5.26 | 6.81 | 8.63 | 11.40 |
| 80 | 3 | 88.9 | 4.51 | 6.45 | 8.37 | 11.30 | 15.20 |
| 100 | 4 | 114.3 | 5.84 | 8.36 | 12.18 | 16.07 | 22.30 |
| 125 | 5 | 141.3 | 9.47 | 11.57 | 16.81 | 21.80 | 31.97 |
| 150 | 6 | 168.3 | 11.32 | 13.84 | 25.36 | 28.30 | 42.70 |
| 200 | 8 | 219.1 | 14.79 | 19.96 | 33.31 | 42.60 | 64.60 |
| 250 | 10 | 273.1 | 22.63 | 27.78 | 41.77 | 60.50 | 96.00 |
Four sectors widely use this material, and each one draws on a different part of the austenitic grade range.

Refinery process units route hydrocarbons through heater piping, overhead lines and transfer headers. Stabilised 321 holds the sensitisation window at heater outlets, while 316L handles corrosive overhead condensate.

Crackers and aromatics complexes carry hot process streams with chloride and organic acid exposure. Grades 316, 316Ti and 904L are specified across reactor loops, quench circuits and acid dosing runs.

Gas sweetening and chemical synthesis units expose piping to amine solutions, sulphur compounds and wet acids. Molybdenum-bearing grades resist the chemistry where plain chromium-nickel material pits.

Steam headers and superheater connections sit at creep temperature for years. High-carbon 321H and 347H keep stress rupture strength there, backed by IBR certification where the statute applies.
As a trusted SS EIL approved pipes supplier, we ensure EIL-approved stainless steel pipes arrive safely, fully certified, and securely packaged worldwide.
Buyers return to Moonlight Tubes for certified material, approved grades and stock that ships on schedule. Every order is backed by documented quality, a wide size range and delivery commitments we hold to.
EIL Approved means the pipes come from a vendor enlisted with Engineers India Limited and can be procured for projects that consultancy engineers.
How is a vendor confirmed on the Engineers India Limited approved vendor list? Confirmation is made against the project's enlistment records, and we submit our approval documentation with every offer.
EIL issues the piping material specification for each project, and its austenitic stainless classes reference ASTM A312 / ASME SA-312 for the pipe.
Eleven grades are available in EIL Approved stainless steel pipes: 304, 304L, 310, 316, 316L, 316Ti, 321, 321H, 347, 347H and 904L.
EIL Approved SS pipes are supplied in seamless and welded form, including ERW, since ASTM A312 accepts any automatic welding process that adds no filler metal. The specification also covers heavily cold-worked pipe.
EIL Approval is a vendor enlistment governing refinery and petrochemical procurement, while IBR Approval is a statutory certification for boiler and steam service under the Indian Boiler Regulations, 1950, framed under the Boilers Act, 1923.